EN

Processing performance is paramount to any large-scale operation in the fast-paced world of industrial filtration. From beverage filtration and chemical separation to water purification, demanding processes require a filtration medium that can deliver consistent results under heavy throughput. Diatomite powder – derived from the fossilized diatomic shells formed from sedimentary rock, has emerged as the material of choice for these large-scale operations.
Its exceptional porous structure and chemical inertness deliver unparalleled advantages in clarity, flow rate, and operational economy. Runhuabang utilizes leading-edge processing to formulate diatomite powders that fit this critical industrial need and help make short work of large-scale filtering.
The Unique Physical Structure That Drives Performance
The real power of diatomite powder lies within its microscopic profile. Each particle is a highly complex skeletal structure riddled with literally billions of tiny pores and convoluted channels - a structure derived directly from the cell walls of prehistoric diatoms. The most immediate benefit of this micro-architecture is its extraordinary level of porosity and extremely low bulk density. In an industrial filter aid, such particles will interlock to form a rigid but permeable cake that acts as a deep bed filter.
Unlike surface filtration that blinds easily, diatomite’s cake effectively captures solids throughout its depth, giving an extremely high dirt-holding capacity and extend the cycle time between cleaning or replacement. The structure's inherent rigidity keeps the cake stable under pressure, preventing it from compacting and ensuring it maintains an excellent flow rate even in a high-volume process.
Enhancing Flow Rates and Reducing Energy Consumption
One of the most significant economic benefits of employing diatomite powder in a large-scale filtering process is the exceptional clarity that can be achieved without sacrificing the flow rate of the filtration liquid. Because the complex matrix of channels forms a tortuous pathway, solids are trapped within the diatomite cake while liquid passes with minimal resistance, creating a much lower pressure drop compared to other types of media. For large facilities with flow rates of thousands of liters an hour, this reduction in differential pressure translates to tremendous savings in pumping energy.
In addition to lowering energy costs, high flow rate capacities mean that companies can process greater quantities of product through the filters, reduce downtime and save on labor and filter disposal expenses.
Runhuabang works to optimize the balance between product clarity and efficient flow rate with its diatomite powders for the good of your bottom line.
Rigorous Quality Control for Industrial Reliability
In industrial filtration, large-scale processors simply can’t risk inconsistent performance. Poor quality or varying sizes in filter aid can mean disrupted batches, sub-par product quality, damaged equipment, and production stoppages. Runhuabang takes quality control very seriously at all stages of production.
With over 20 testing instruments in our state-of-the-art facility, and a technical team of well-trained researchers in addition to highly qualified staff, we monitor everything that goes into our product, from raw materials to final packaging. Each batch is rigorously inspected for things like pH, moisture content, and particle size distribution to ensure they meet rigorous industry standards. This ensures that when a large facility uses Runhuabang diatomite powder, they can rest assured it will perform predictably and protect the integrity of their end product.
Versatility Across Diverse Industrial Applications
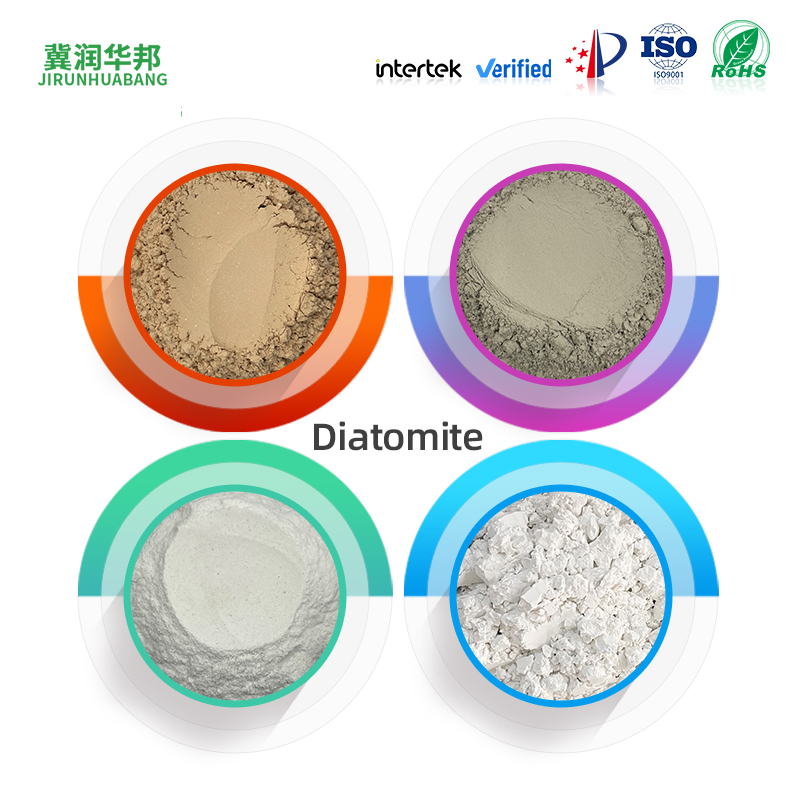
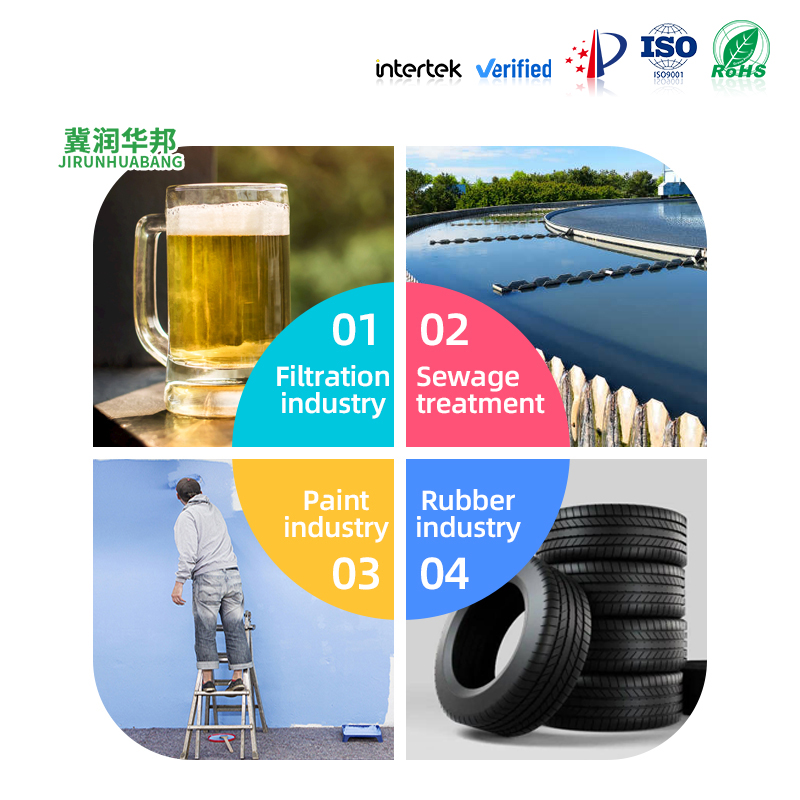
Runhuabang offers a range of diatomite grades and processing methods to meet the specialized needs of dozens of industrial filtering applications worldwide. From producing pristine fruit juices and wines to providing ultra-clean drinking water and filtering catalysts out of chemical processes, diatomite has the flexibility to tackle it all. It is the favored option for making crystal clear beers and fruit-based beverages because it removes yeast and fine particles without impacting color or flavor. In water treatment, it helps to eliminate suspended particles and microorganisms.
Chemical and oil filtration are two other critical applications where diatomite excels, as its chemical inertness prevents any interaction with the filtrate. As a leading supplier of non-metallic mineral products for more than 25 years, Runhuabang’s solutions are helping industries across the globe – in North America, Southeast Asia, and beyond – get better at filtering.